Powder Coating Line
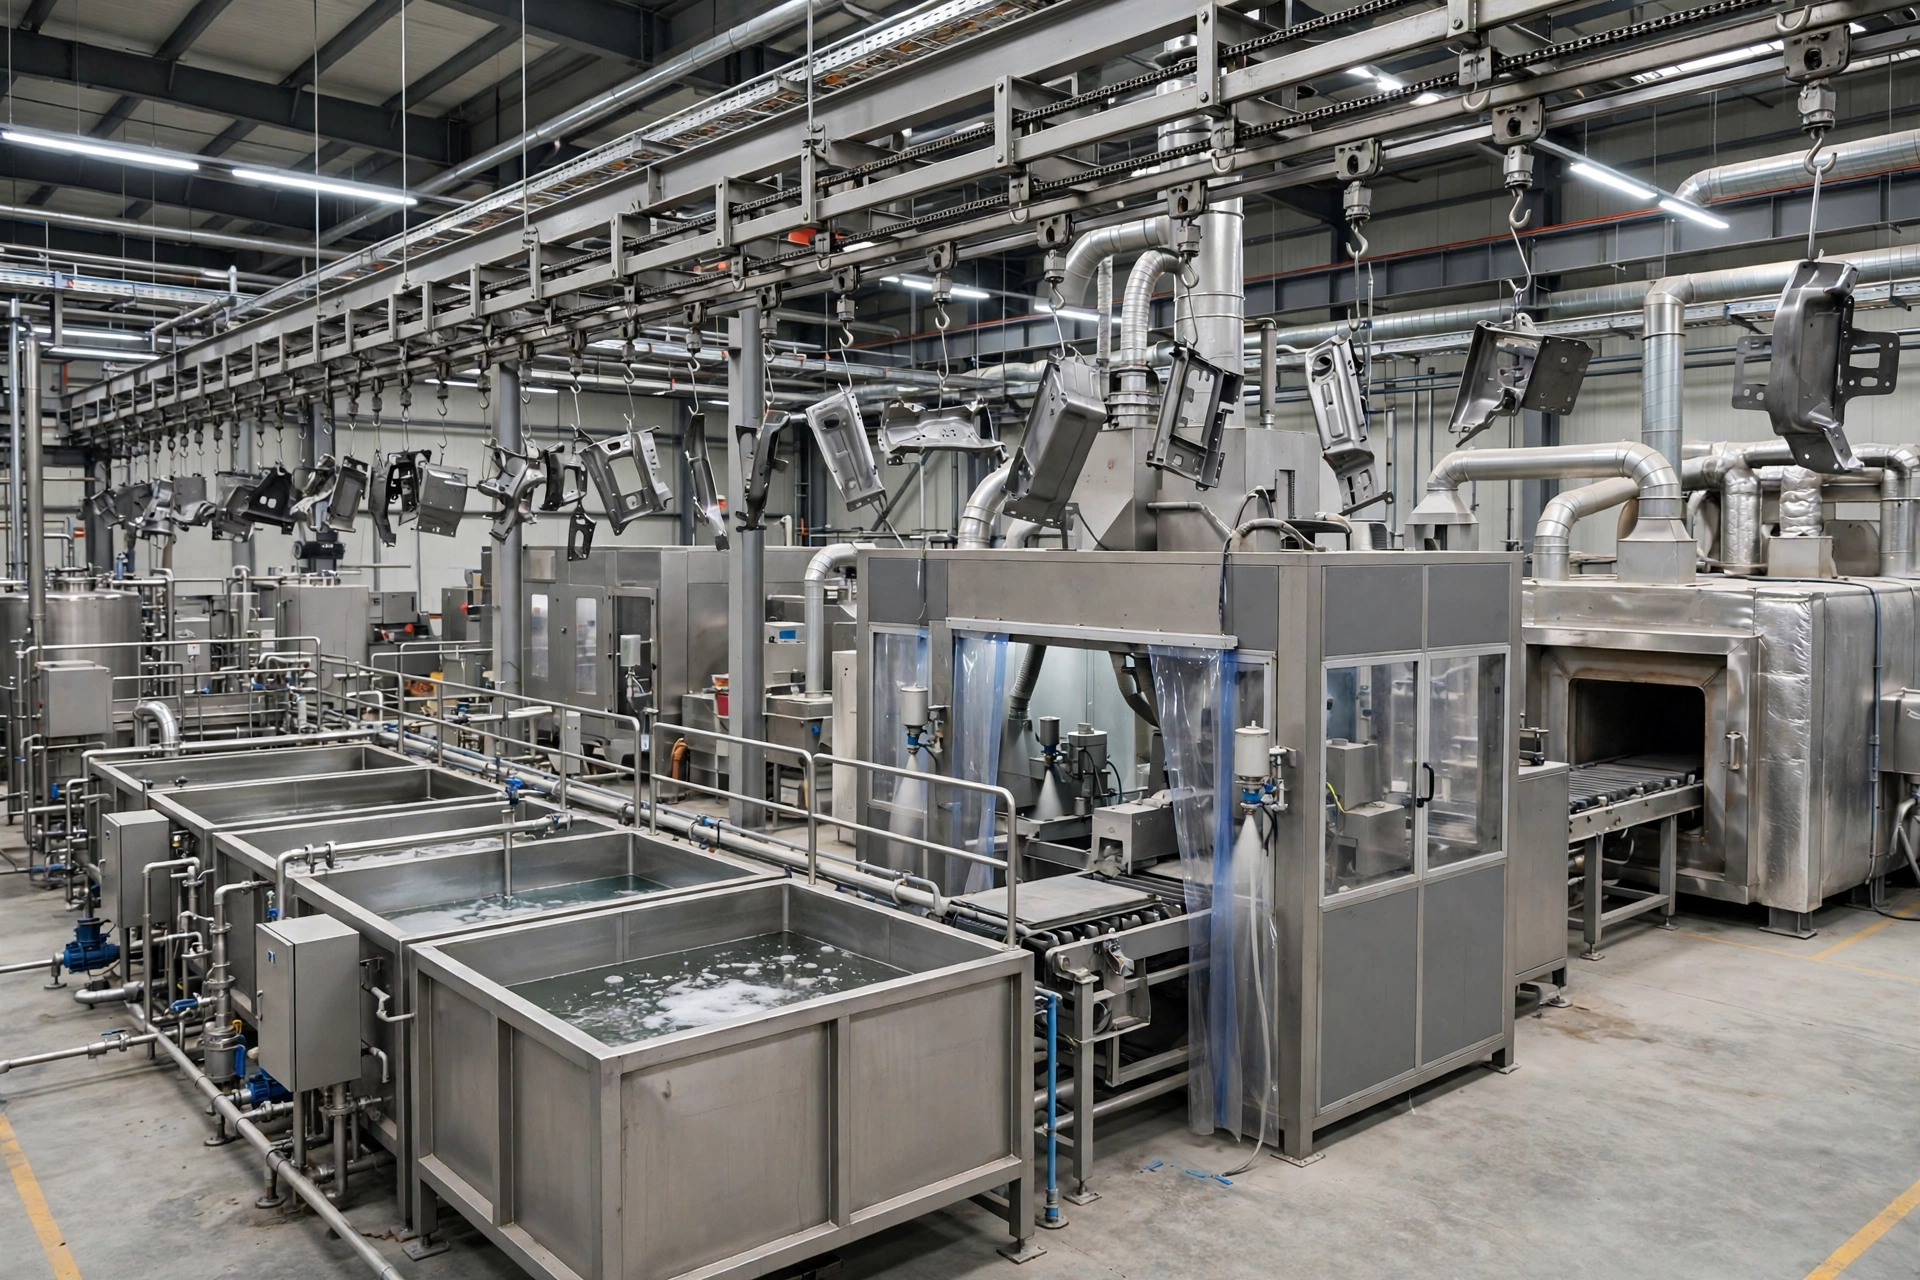
A powder coating line sprays dry powder electrostatically and cures it into a hard film. Lynvex powder lines combine pretreatment, a powder booth, and a curing oven on an overhead conveyor, configured to your parts and output.
Home › Powder Coating Line
A powder coating line sprays dry powder electrostatically and cures it into a hard film. Lynvex powder lines combine pretreatment, a powder booth, and a curing oven on an overhead conveyor, configured to your parts and output.
The process runs nine steps: loading, degreasing and surface pretreatment, drying, electrostatic powder spraying, curing, cooling, inspection and unloading, on a conveyor that carries parts through every stage. Curing is typically 185 degrees for 15 minutes; your powder supplier's schedule governs the final oven setting.
| Stage group | Steps |
|---|---|
| Pretreatment | Degrease, rinse, surface conversion, dry-off |
| Application | Electrostatic powder spraying in the booth |
| Curing | Oven cures the powder film (typically 185°C for 15 minutes) |
| Finishing | Cooling, inspection, unloading |
Part size and weight set the conveyor and booth opening; the powder and colour-change rhythm set the booth recovery system; the cure schedule sets the oven. Send all three and the proposal will state line length and layout against your workshop.
This equipment is supplied with a 12-month warranty. Spare wear parts (guns, nozzles, filters, belts) are listed in the quotation so you can stock them at commissioning.
Complete lines serve factories where coating is a core process rather than a side station: metal furniture and hardware, plastic housings at volume, building components and mixed production that runs all day. The line's value is flow — parts enter raw and leave finished, with no trolleys of half-done work waiting between a booth here and an oven across the building.
Line projects fail on interfaces, not on individual machines: conveyor hand-offs, booth openings, oven entry seals and control handshakes between sections. That is why a line proposal states every section's size and the spaces between them, and why the layout is drawn against your workshop before prices are fixed.
Two routines protect a line's output. The first is loading discipline: hangers and fixtures must present parts at the spacing the spray programs assume, or film build varies along the line. The second is staged cleaning: booths, guns and oven filters each have their own interval, and a single missed interval usually shows up as finish defects a shift later. Commissioning includes a maintenance schedule per section, sized to your coating and shift pattern.
They depend on the booth recovery type chosen at configuration. State your colours per day and we will specify accordingly.
Send your part drawings, part size and output target. We will confirm the machine or line configuration and reply with a quotation.