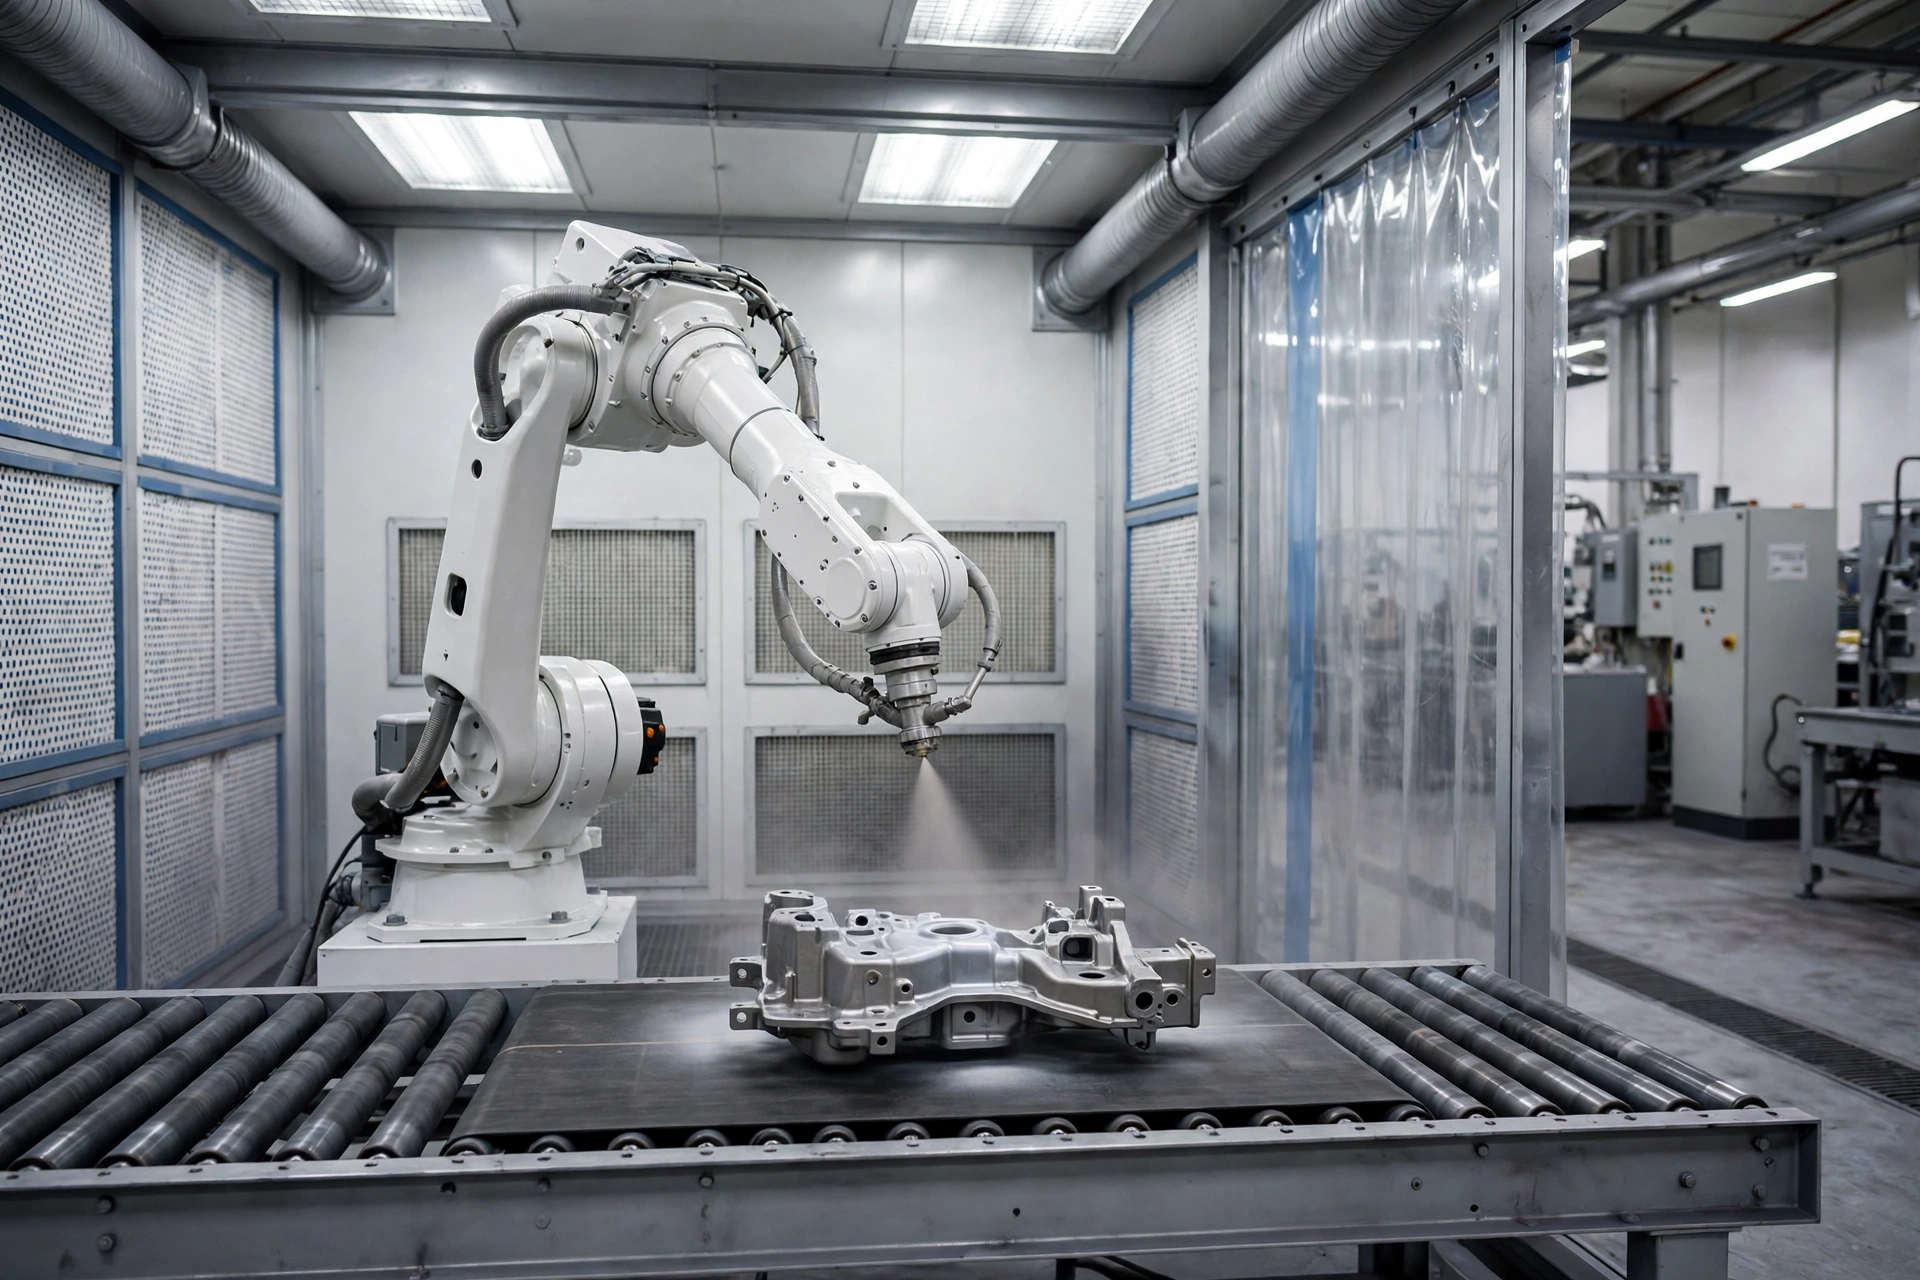
Robot or reciprocating machine?
A reciprocating machine repeats one stroke pattern: cheap, fast and ideal for flat or gently curved parts that never change. A six-axis robot reproduces a taught path around edges, recesses and undercuts, and a new part family usually means a new program, not new hardware. The break-even question is variety: the more part families and shape changes you run, the stronger the case for the robot.
| Factor | Reciprocating machine | Spray painting robot |
|---|
| Part shapes | Flat and simple curves | Complex 3D shapes, recesses, edges |
| Changeover | Adjust stroke and fixtures | Load a stored program and change fixtures |
| Programming | Mechanical settings | Teach pendant or offline program per part family |
| Typical role | Dedicated high-volume part | Mixed production, several part families |
What a robotic installation includes
Beyond the robot itself, a working cell needs a booth with extraction sized to the robot envelope, part fixtures or a conveyor that presents parts repeatably, a paint supply unit and a safety zone. Lynvex robotic lines are configured around your largest part and your takt time; the robot detail page lists the robot parameters for this line configuration.
Application scope
Robotic spraying serves parts whose geometry defeats fixed guns: deep-drawn trim, housings with recesses, doors with moulded profiles, sanitary ware and mixed families sharing one cell. The robot's taught path keeps gun distance and angle on surfaces that change orientation continuously, which is exactly where manual spraying varies most between operators and shifts.
A robot cell also changes the labour equation: operators load, unload and inspect instead of spraying, and exposure to paint mist falls. For factories facing painter shortages or strict exposure rules, that is often the deciding argument alongside finish consistency.
Teaching and changeover
A new part family needs a taught program and a fixture that presents the part repeatably; after that, changeover is a program call and a fixture swap. Teach time depends on part complexity, and it is spent once — which is why the business case improves with every family added to the cell. When you request a quote, list families in launch order so commissioning teaches the highest-volume parts first.
What to send for a configured quotation
- Part drawings or photos, with the largest part size (L x W x H)
- Coating type and finish requirements (colour, gloss, film thickness if specified)
- Required output: parts per hour or per shift, and working hours per day
- Destination country and local power supply (voltage / frequency)
- Workshop space available for the machine or line, if a full line is planned
Buyer questions
Do I need robot programming experience?
No. Programs for your launch parts are set up as part of commissioning, and your team is shown how to teach new points. List your launch part families in the inquiry.
Can the robot share a booth with manual spraying?
Layout and safety rules decide this. Send your booth dimensions and we will check the cell layout.
Not sure which configuration fits?
Send your part drawings, part size and output target. We will confirm the machine or line configuration and reply with a quotation.
Send an Inquiry