Electrostatic Powder Coating Guide
Electrostatic powder coating uses an electric charge to draw powder onto the part before curing. This guide explains the charge, spray and cure stages and what a complete powder coating line includes.
Home › Electrostatic Powder Coating Guide
Electrostatic powder coating uses an electric charge to draw powder onto the part before curing. This guide explains the charge, spray and cure stages and what a complete powder coating line includes.
The spray gun charges powder particles as they leave the nozzle; the grounded part attracts them, and the charge holds the powder in place — including, with the right technique, around edges and into recesses. Powder that misses is collected by the booth recovery system and reused, which is the process's material advantage over liquid paint. Film thickness is controlled by gun settings, distance and pass count.
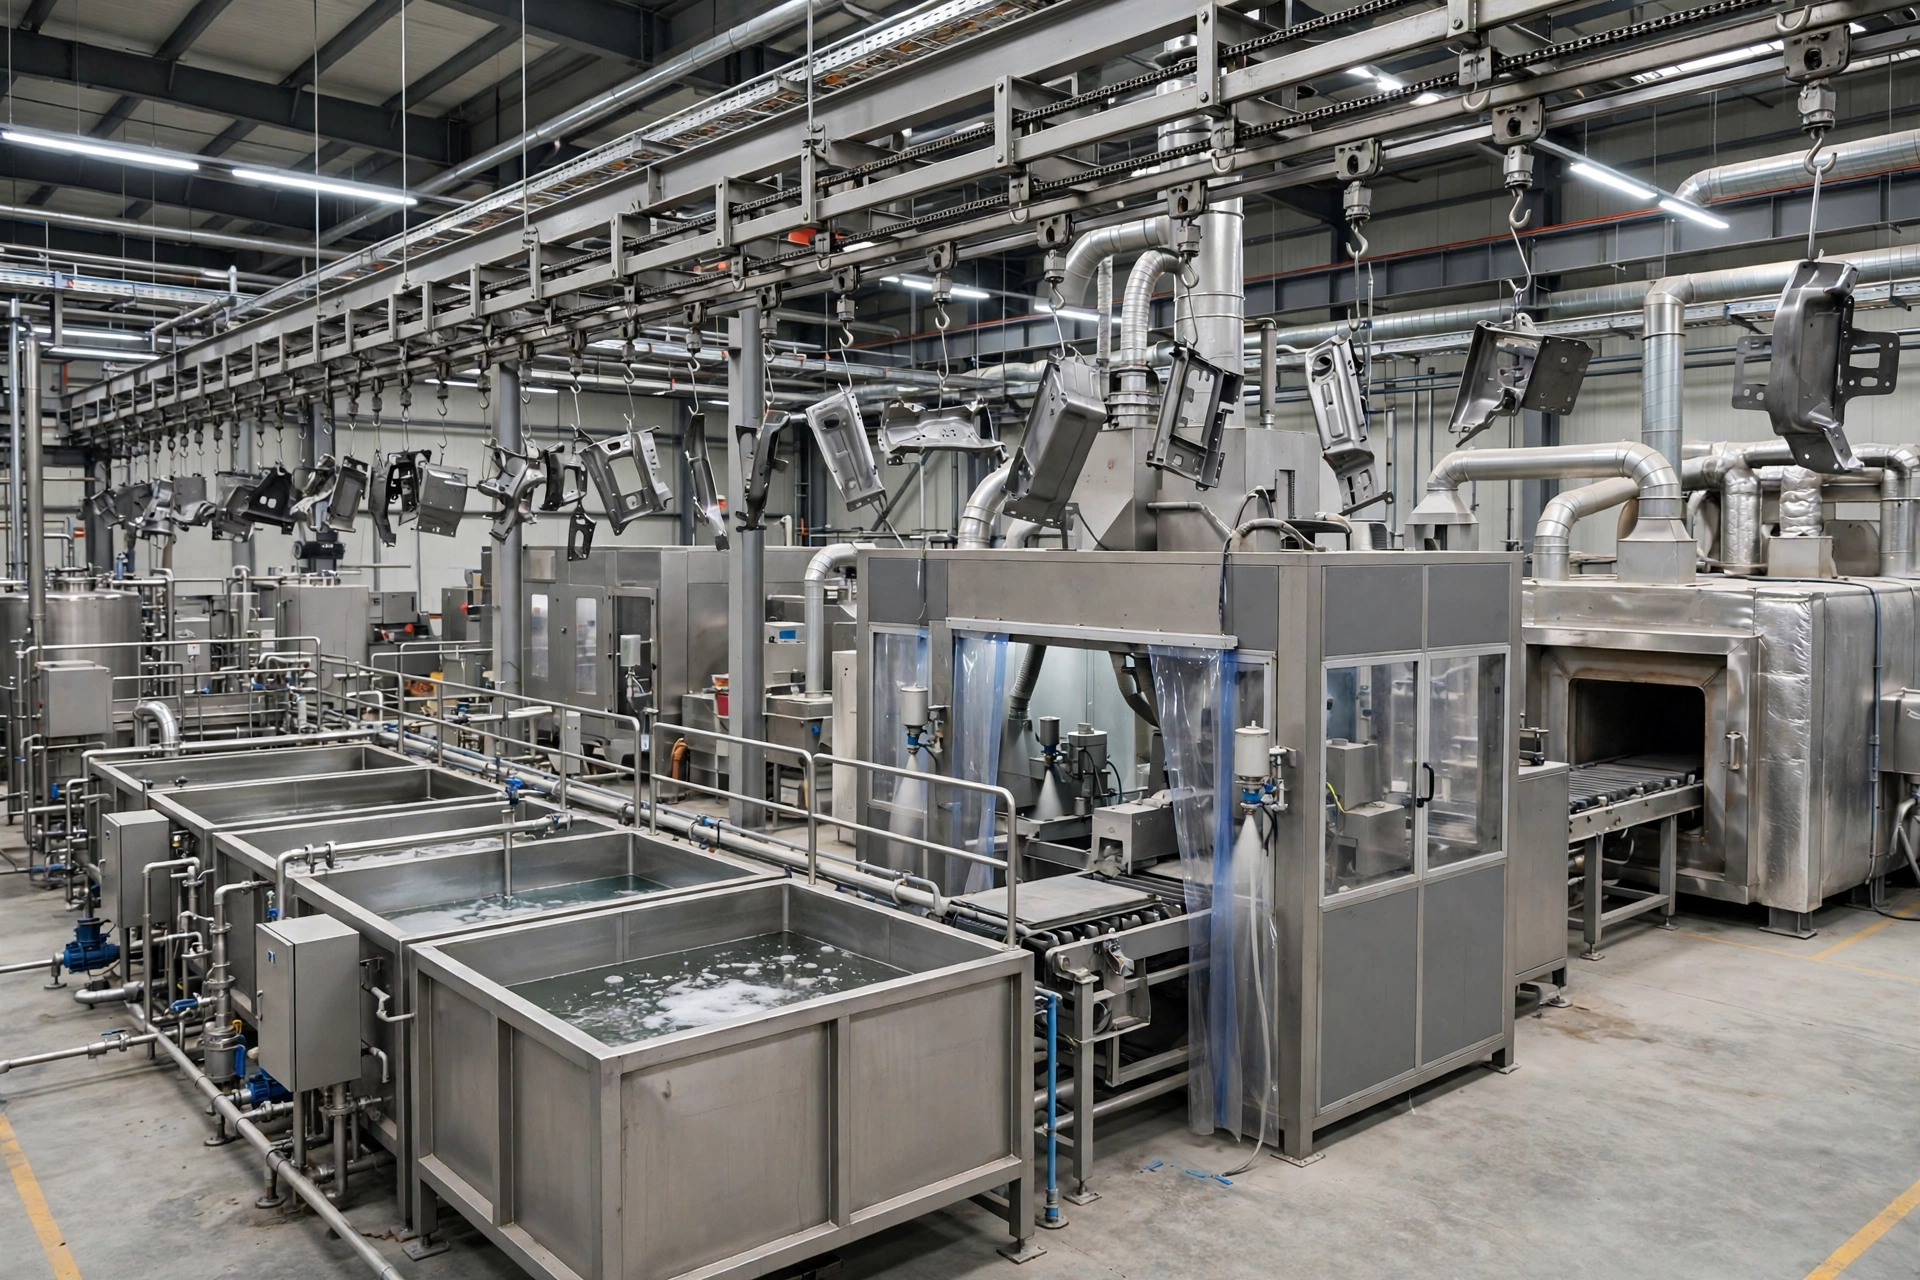
Before spraying, parts are pretreated so the film adheres and resists corrosion; after spraying, the oven melts and cures the powder into a continuous film at the powder supplier's schedule. A complete line therefore includes pretreatment, a dry-off stage, the powder booth, the curing oven and the conveyor joining them — each stage sized to the largest part and the line's takt.
Electrostatic application stands or falls on grounding. Parts hang on hooks that accumulate cured powder, and a poorly grounded part repels the very powder the charge is meant to attract — wrap falls, coverage thins and Faraday-cage areas starve. Hook cleaning and ground checks are therefore scheduled maintenance on a powder line, not housekeeping.
Electrostatic attraction works against you in inside corners and deep channels: charged powder arriving at a recess meets a weakened field and deposits thinly — the Faraday cage effect. Experienced powder coaters answer with gun settings, lower charge for recess passes, gun angle and sometimes a manual touch-up station for the worst geometries. A line proposal that promises perfect recess coverage from charge alone is overselling; ask how your deepest recess will be handled and judge the answer.
The same honesty applies to colour: powder overspray is recyclable within one colour, so frequent colour changes carry cleaning time that belongs in the line's rate calculation from the start.
Send part drawings, coating type and output target through the inquiry page; the reply will confirm the configuration and quotation.
Send your part drawings, part size and output target. We will confirm the machine or line configuration and reply with a quotation.